Uttam Industries — Railway Industry Welding Machine Manufacturer since 1965 Mandi Dabwali, Haryana & Delhi, India  |  Global Export Enquiries Welcome
Engineering Excellence Since 1965 · Heavy Infrastructure & Rolling Stock

Railway Industry Welding Machine: Global Engineering Procurement & High-Duty Fabrication Guide

A comprehensive technical authority guide for international procurement directors, railway maintenance engineers, and rolling stock fabricators. Discover EN 15085 & ISO 3834 compliant welding systems engineered for extreme duty cycles, structural fatigue resistance, track joining, bogie fabrication, and next-generation high-speed rail infrastructure.

EN 15085-2 / ISO 3834 Ready 100% Copper Winding & Full Load Tested 380V - 440V Multi-Voltage Export Units 60 Years Manufacturing Integrity
60Years in heavy arc engineering
100%Class H copper transformer windings
130–1250AHigh duty cycle output range
6 ContinentsGlobal rail & fabrication exports
User Intent & Industry Standards

Why Railway Industry Welding Demands Zero-Defect Metallurgical Integrity

Railway infrastructure and rolling stock operate under severe, continuous dynamic loads, multi-axial vibration, atmospheric exposure, and thermal expansion cycles. A single structural failure in a rail joint, bogie frame, or locomotive underframe can result in catastrophic derailments and millions of dollars in network downtime.

Global procurement teams searching for a high-performance Railway Industry Welding Machine require far more than generic welding specs. They need absolute assurances regarding melt-through prevention, grain structure stability in high-tensile steels (such as S355J2W, S460M, and rail grades R260/R350HT), precise penetration depth, and full compliance with EN 15085-2 (Class CL1 to CL4) and ISO 3834-2 requirements.

  • Dynamic Fatigue Protection: Synergic pulse waveforms eliminate micro-porosity and undercut in critical load-bearing bogie seams.
  • High Duty Cycle under Ambient Extremes: Rated for continuous operation at 40°C to 55°C ambient temperatures in desert or tropical rail corridors.
  • Field-Generator Tolerance: Heavy-duty primary power filtering prevents arc drift during trackside repair off temporary diesel gensets.
  • Digital Traceability: Real-time voltage, amperage, and heat input logging to satisfy railway authority compliance audits.
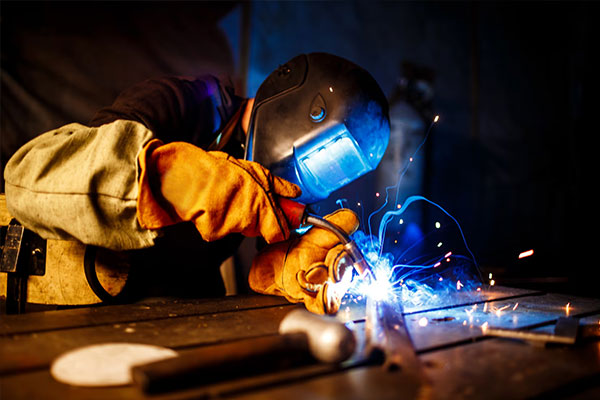
Industrial welder operating heavy duty railway industry welding machine on structural steel rail component
1965Manufacturing Heritage
Product Recommendations

Engineered Railway Industry Welding Machine Portfolio

Six specialized machine classifications designed by Uttam Industries to meet the stringent structural, trackside maintenance, and coach fabrication needs of modern rail networks.

Bogie & Heavy Frame Fabrication

Multi-Process MIG/MAG Railway Welder (500A Synergic Pulse)

Specifically tuned for welding thick-section carbon steels and weathering steel bogie side-frames. Features synergic pulse control that eliminates spatter, reduces post-weld grinding by 80%, and maintains uniform root fusion without cold lap defects.

Current Range: 50A – 500A (100% Duty Cycle at 400A) Wire Feed: Heavy 4-roll geared feeder for 1.2mm – 1.6mm solid/flux-cored wire Rail Standards: EN 15085 CL1 / CL2 joint suitable Primary Input: 380V / 415V / 440V 3-Phase 50/60 Hz
Trackside & Site Repair

Double Holder Heavy Duty ARC Welding Machine (Twin 400A / 600A)

A flagship Uttam Industries design engineered for railway workshops and track repair teams. Utilizes a massive dual-wound transformer core allowing two operators to weld simultaneously with completely independent amperage control without voltage sag.

Current Range: Dual 50A – 400A or Dual 50A – 600A Winding Material: 100% Electrolytic Class H Copper Vanguard Feature: Generator-friendly wide input tolerance Application: Turnout maintenance, rail building-up, site steelwork
Passenger Coach & Tanker Car

Precision AC/DC TIG Rail Welder (300A – 400A High Frequency)

Engineered for stainless steel passenger coach sidewalls, aluminum alloy roof structures, and pneumatic braking pipework. High-frequency arc striking ensures zero tungsten contamination, while pulse frequency control limits thermal warping on thin gauge metals.

Current Range: 10A – 400A AC/DC Pulse Pulse Frequency: 0.5 Hz – 500 Hz adjustable Water Cooling: Integrated closed-loop torch cooling unit Application: Metro car shells, stainless tanks, hydraulic lines
Fastener & Earth Bonding

Capacitor Discharge Stud Welding Machine (M3 – M16 Capacity)

Delivers single-sided, millisecond-fast welding of insulation pins, electrical earthing bosses, and cable conduit brackets to rail car bodies without burning through interior painted surfaces or reverse-side cosmetic finishes.

Stud Diameter: M3 to M16 (Threaded studs & shear connectors) Weld Time: 1 – 3 milliseconds micro-processor controlled Portability: Heavy-duty wheeled chassis with gun holster Application: HVAC cladding, electrical grounding, interior panels
Sub-Assembly & Rail Jointing

Heavy Duty ARC Welding Rectifier & SAW Power Source (800A – 1250A)

Built for continuous heavy structural fabrication, automated submerged arc welding (SAW) of longitudinal girder seams, and high-deposition hardfacing of rail frogs and switch points subjected to severe impact loading.

Current Range: 100A – 1250A Heavy Rectifier DC Duty Cycle: 100% Continuous Duty Cycle at Maximum Rating Protection: Thermal overload cut-outs & sealed electronics Application: Heavy bridge girders, switch frogs, longitudinal beams
Automated Plate Profiling

CNC Fiber Laser & Heavy Air Plasma Cutting Machine

Complements railway welding lines by producing precision bevel-cut steel plates and bogie web plates ready for immediate joint fit-up without manual grinding. Eliminates edge micro-cracking prior to welding.

Laser Output: 3kW – 12kW Fiber Laser / 200A Plasma Table Format: Customizable gantry up to 3m x 12m plate size Bevel Cutting: V, Y, and K-bevel capability for full weld penetration Application: Bogie plates, buffer beam gussets, wagon chassis
Engineering Selection Matrix

Railway Industry Welding Machine Process Comparison

A quick engineering baseline used by global rail procurement teams to align machine specifications with component thickness, EN 15085 weld performance classes, and output requirements.

Technical guidance for railway equipment procurement. Specifications can be tailored by Uttam Industries' engineering team based on local grid conditions and OEM standards.
Process & Machine Type Railway Application Area Material Thickness EN 15085 Class Deposition Rate Procurement Action
Synergic Pulse MIG/MAG (500A) Bogie frames, cross beams, coupler pockets 4.0 – 25 mm CL1 / CL2 Very High (4.5 – 8.5 kg/h) Get a Quote
Double Holder ARC Welder (Twin 400A) Yard maintenance, trackside structural welding 3.0 – 40 mm CL2 / CL3 Moderate (1.8 – 3.2 kg/h) Get a Quote
AC/DC HF Pulse TIG (400A) Stainless metro shells, aluminum roofs, brake pipes 0.8 – 8.0 mm CL1 / CL2 Precision Low (0.8 – 1.5 kg/h) Get a Quote
Stud Welding Unit (M3-M16) Earthing bosses, insulation pins, wire tray mounts Studs 3 – 16 mm CL3 / CL4 Fastener Instant (10-20 studs/min) Get a Quote
SAW / Heavy Rectifier ARC (1000A) Longitudinal wagon girders, rail frog build-up 12.0 – 60+ mm CL1 Ultra High (9.0 – 18 kg/h) Get a Quote
CNC Plasma / Laser Cutting Gantry Bogie web plate profiling, buffer gusset prep 0.5 – 40 mm Cutting / Prep High Speed (up to 12m/min) Get a Quote
Market Analytics & Strategic Foresight

Future Procurement Trends in the Global Railway Welding Equipment Market

Insights compiled for procurement managers, EPC contractors, and railway authority buyers navigating the next decade of rail infrastructure modernization.

1. Accelerated Shift toward High-Inverter Efficiency & Power Factor Correction (PFC)

Global rail operators are enforcing strict decarbonization mandates across workshop facilities. Legacy transformer welders with poor power factors (0.60–0.70) are rapidly being phased out in favor of IGBT inverter-based Railway Industry Welding Machines featuring active Power Factor Correction (PFC > 0.95). These systems reduce overall electrical energy consumption by 30% to 45% during continuous production cycles, significantly lowering operational expenditures for heavy rolling stock factories.

2. Mandated Industry 4.0 IoT Parameter Logging for Auditability

Under revised international rail safety standards (such as EN 15085-2 edition 2020), every critical weld joint on passenger trains must be digitally traceable. Future procurement tenders prioritize welding power sources equipped with integrated IoT sensors, Ethernet/Modbus connectivity, and weld-data logging modules. These track arc voltage, current, wire feed speed, and total heat input in real-time, instantly flagging any parameter deviation to quality engineers before the bogie leaves the assembly bay.

3. Multi-Voltage & Generator-Adaptive Systems for Trans-National Freight Corridors

Cross-border rail networks, such as the Belt and Road transit lines, North American freight links, and Pan-African corridors, often present vastly different electrical grid environments (ranging from 380V 50Hz to 480V 60Hz or unstable trackside diesel generator supplies). Procurement buyers are actively standardizing on heavy-duty multi-voltage units engineered with wide-tolerance line compensation technology to prevent machine burnouts during remote track maintenance.

4. Hybrid Laser-Arc Welding (HLAW) Adoption for High-Speed Rail Shells

As passenger rail speeds push beyond 300 km/h, lightweighting passenger coach bodies using thin-wall stainless steel and aluminum extruded profiles becomes paramount. High-Speed Rail (HSR) manufacturing centers are incorporating Hybrid Laser-Arc Welding systems—combining deep laser penetration with MIG arc gap-bridging—to achieve seamless 10-meter longitudinal joints with virtually zero post-weld distortion.

Technological Innovations

Industry Development Trends in Railway Infrastructure & Rolling Stock Welding

How modern metallurgy, digital control, and robotics are reshaping the manufacturing lifecycle of locomotives, freight cars, and continuous welded rails (CWR).

Advanced Waveform Control in GMAW-P

Modern inverter power sources continuously modify current waveforms microsecond-by-microsecond. For railway bogie fabricators, this allows controlled metal transfer during pulsed MIG welding, completely preventing cold laps on thick plates while preserving impact toughness down to -40°C ambient temperatures.

Continuous Flash Butt Welding (FBW) Progress

For Continuous Welded Rail (CWR) tracks, mobile track-bound Flash Butt Welding machines are replacing traditional thermit welding. FBW systems deliver solid-state forge welds with zero filler metal, matching the mechanical properties of the parent rail steel and dramatically reducing track-joint maintenance frequencies.

Robotic Welding Cells with 3D Vision Seam Tracking

Tier-1 rolling stock suppliers are increasingly replacing manual stick welding on coach underframes with multi-axis gantry robots integrated with 3D optical seam trackers. Uttam Industries' welding power units readily interface with robotic controllers to deliver high-speed, repeatable, 100% inspectable fillet welds.

Integrated Thermal Stress Mitigation Technology

Advanced railway welding systems now incorporate controlled pre-heat monitoring and controlled interpass temperature protocols. This prevents martensitic phase transformation and hydrogen cracking in high-strength low-alloy (HSLA) structural steels used in heavy haul mineral wagons.

Enterprise Advantage & E-E-A-T

Why Global Railway Contractors Trust Uttam Industries

Rooted in 60 years of heavy industrial transformer and welding equipment manufacturing in Mandi Dabwali, Haryana & Delhi, India.

Uttam Industries manufacturing plant full load testing and quality control process for railway industry welding machines
100 percent copper transformer winding icon

100% In-House Electrolytic Copper Winding

Unlike light-duty commercial welders that utilize aluminum windings with synthetic insulation, every heavy-duty Uttam Railway Industry Welding Machine is wound in-house using high-purity electrolytic copper wire with Class H varnish insulation, guaranteeing maximum thermal headroom and decades of continuous service.

Full load testing icon

100% Full-Load & Burn-In Testing Protocol

Prior to dispatch, every single machine undergoes rigorous full-load testing on resistive dummy loads at maximum rated output, followed by insulation resistance, dielectric withstand, and temperature rise checks. Serial-linked test certificates are provided with every export shipment.

Custom engineering and OEM support icon

Application-Specific Engineering & Customization

We build tailored equipment variants featuring custom primary voltage taps (220V–440V), extended interconnecting cable looms up to 50 meters, heavy-duty rubberized wheels for rugged rail tracks, water-cooled torch packages, and specialized remote current pendants.

Export packing and spare parts support icon

Independent Overseas Maintenance Support

We equip overseas railway maintenance teams with non-proprietary, easily replaceable components, detailed wiring schematics, multilingual operating manuals, and structured 2-year recommended spare parts packages to ensure total operational self-reliance.

Proven Reliability

Built to Be Judged on Rail Workshop Uptime

Direct factory manufacturing, transparent technical parameter rating, and comprehensive export crating.

Quality inspection and load testing of heavy duty railway industry welding machines

Rigorous Industrial Validation Before Dispatch

Every unit leaving our facilities in Mandi Dabwali, Haryana or Delhi is subjected to high-current load testing, open-circuit voltage calibration, and severe thermal soak checks. We verify arc stability across standard and non-standard input voltages so your workshop experiences zero startup delays.

  • 100% full-load and short-circuit protection testing
  • Earth continuity and high-voltage breakdown insulation checks
  • Documented test reports attached to each machine's serial number
Experienced welding engineering team supporting railway customers

Six Decades of Heavy Engineering Specialization

Since 1965, Uttam Industries has engineered welding power sources for railway workshops, shipyards, steel rolling mills, and automotive tier-1 suppliers. Our engineers advise you on exact wire selection, shielding gas ratios, and duty cycle headroom before you issue a PO.

  • Deep technical consultation on EN 15085 weld procedure specifications (WPS)
  • Custom transformer design for high-ambient operating environments
  • Direct engineer-to-engineer parameter selection support
Cost efficient industrial railway welding machine equipment

Modular Architecture for Low Lifecycle Maintenance

We eliminate proprietary single-board microchips that lock you into expensive OEM service calls. Our machines use modular, heavy-duty industrial contactors, heavy-gauge copper windings, and standardized torches available in over 100 countries.

  • Modular component layout for fast field troubleshooting
  • Standardized Euro-connector torches and DINSE cable plugs
  • Comprehensive recommended spare parts kit included with export orders
Packing and dispatch of railway welding machines for export

Robust Wooden Crating for International Sea Freight

Export consignments are secured inside fumigated, heavy-duty wooden crates lined with moisture barrier foils and silica desiccant packs. Machines arrive on-site fully calibrated, undamaged, and ready for immediate connection.

  • Fumigated ISPM-15 compliant timber packaging
  • Vapor Corrosion Inhibitor (VCI) protective wrapping
  • Complete wiring schematics and user manuals included in every crate
Verified Customer Reviews

What Industrial & Railway Fabricators Say

Manoj Kumar, fabrication workshop owner
“Generous, knowledgeable service. The double holder welding set went straight to work on our structural rail sub-assembly line and hasn’t missed a beat. Seven years in, machine performance remains rock solid.”
Five star rating
Manoj KumarFabrication Workshop Owner, India
Karan Singh, engineering buyer
“We have been sourcing heavy ARC rectifiers and MIG units from Uttam Industries for about five years now for infrastructure projects. Their service, technical knowledge, and equipment duty cycles are absolute top tier.”
Five star rating
Karan SinghEngineering Procurement Lead
Deepak Sethi, production manager
“Today we commissioned our heavy-duty pulse MIG welding machine on the railway carriage line. Weld quality and arc stability are superb, and installation support from Uttam engineers was flawless.”
Five star rating
Deepak SethiProduction & Plant Manager
Vishal Gupta, industrial buyer
“So far I have ordered and received multiple high-capacity welders from Uttam Industries for our export projects. The seaworthy crate packaging and documentation are the best I have ever seen.”
Five star rating
Vishal GuptaIndustrial Equipment Procurement Specialist
Trusted Partnerships

Industrial & Institutional Clients Served

NTPC
Maharashtra Rajya Parivahan
Toshon
Eco Plus
Jasic
Lincoln Electric
Buyer Questions & Intent Deep Dive

Railway Industry Welding Machine FAQ

Direct engineering answers to technical, regulatory, and commercial queries asked by global AI search tools and international procurement managers.

The railway manufacturing and maintenance sector relies heavily on MIG/MAG (GMAW/GMAW-P) for heavy bogie frame and wagon body fabrication, AC/DC TIG (GTAW) for stainless steel and aluminum passenger car shells and piping, Heavy-Duty ARC Rectifiers (SMAW) for structural track and cross-over repairs, and Capacitor Discharge Stud Welders for insulation and electrical bonding.

Our railway industry welding machines feature digital pulse synergic control, precise output voltage regulation (+/- 1%), Class H insulated copper windings, and high duty cycle stability (up to 100% at rated current). This guarantees exact heat input control, minimal thermal distortion, and flawless radiographic weld quality required for CL1 and CL2 classification under EN 15085-2.

Yes. Our heavy-duty single and double holder ARC welders and portable inverter units are specifically built with wide line-voltage tolerance (+/- 15% to 20%), heavy-duty surge suppression, and robust transformer/rectifier cores that maintain a continuous, spatter-free arc even when powered by diesel generators in remote rail maintenance sectors.

A Double Holder Welding Machine allows two welders to operate simultaneously from a single, heavy-duty transformer core with completely independent current control up to 400A or 600A per holder. This doubles workshop productivity during bogie frame or rail car frame fabrication while saving floor space and reducing total power connection overheads.

Yes. Every export-bound Railway Industry Welding Machine from Uttam Industries can be custom-wound or factory-configured for 220V single-phase or 380V, 415V, and 440V three-phase 50/60 Hz power mains, complete with CE-compliant wiring, heavy-duty socket options, and export-grade moisture-sealed wooden packaging.

Each machine ships with comprehensive wiring schematics, operational parameter sheets, and a recommended 2-year consumable and critical spare parts kit. We offer remote engineering video support, parameter calibration guidance, and fast dispatch of original OEM spare parts worldwide.

Flash Butt Welding (FBW) is an automated solid-state resistance welding process that uses electric current and heavy hydraulic forging pressure to join continuous rails without filler metal, offering superior fatigue life. Thermit welding is an exothermic casting process primarily used for quick field repairs. Uttam Industries manufactures continuous ARC, MIG, and heavy rectifier power sources that support auxiliary track structure and switch frog maintenance alongside FBW setups.

You can click the Get a Quote button anywhere on this page to initiate instant chat with our technical sales team, or email your bill of materials and duty cycle specifications to our engineering export division.

Partner with India's Premier Railway Welding Equipment Manufacturer

Share your railway project specifications, material grades, plate thicknesses, and annual production targets. Our senior engineering team will evaluate your application and supply a detailed technical proposal and factory-direct quote.

Works & Head OfficeRailway Crossing, Grand Trunk Road, Mandi Dabwali, Haryana 125104, India
Delhi Sales & Export OfficeShop No. 111, Property No. 4135, 1st Floor, M Rais Market, Gali Shahtara, Ajmeri Gate, Delhi 110006, India
Engineering Consultation HoursMonday – Saturday, 09:30 – 18:30 IST