Technical Sourcing Insight Deep Dive: Evaluating Plasma Arc Physics, Kerf Taper, and Thermal Economics
When global procurement teams evaluate a Metal Processing Plasma Cutter for heavy fabrication, the primary decision matrix involves balancing speed, consumable consumption, electrical efficiency, and edge quality. Unlike basic manual plasma torches, industrial metal processing plasma cutters utilize highly constricted ionized gas streams to achieve narrow kerf profiles and minimal dross formation.
Information Gain: Understanding High-Definition Plasma Arc Physics
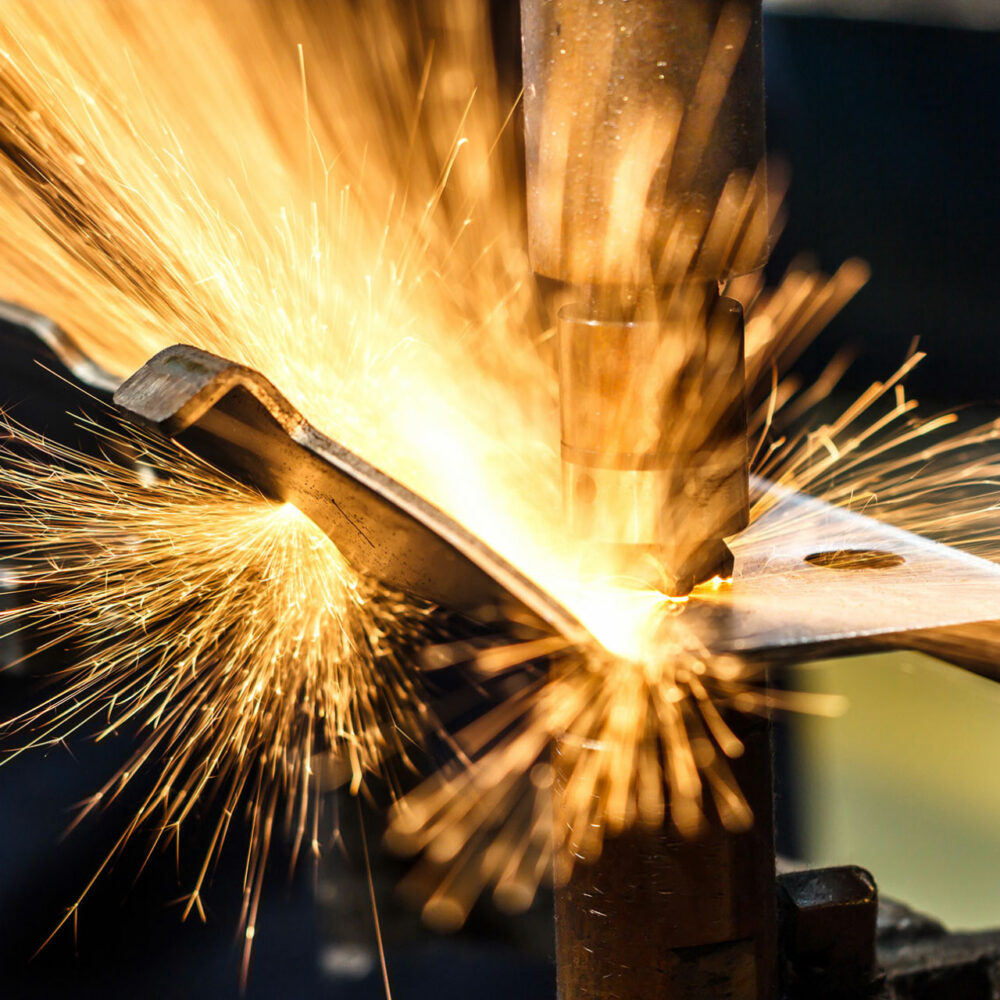
Plasma is created when a neutral gas (such as compressed air, oxygen, or nitrogen) is forced through a narrow nozzle orifice while an electric arc is transferred from a tungsten electrode to the conductive metal workpiece. The electric arc ionizes the gas molecules, creating a superheated conductive plasma jet at temperatures reaching 20,000°K to 30,000°K. Uttam Industries' high-definition torch geometry introduces a secondary swirl gas ring that constricts the arc diameter by up to 50%, dramatically increasing current density and yielding kerf angles under 2 degrees.
1. Kerf Angularity and Edge Geometry Control
In plate profiling, kerf taper (the angular deviation of the cut edge relative to a 90-degree vertical axis) directly impacts assembly time. Excess taper requires secondary machining or manual grinding before butt welding. Uttam Industries integrates advanced torch height sensing with micro-voltage arc monitoring (THC) that adjusts z-axis positioning 50 times per second, maintaining optimum standoff height and securing ISO 9013 Class 3 to Class 4 cut quality.
2. Gas Selection Dynamics for Alloy Processing
Choosing the correct gas mix is critical for optimizing metallurgy and preventing oxidation during metal processing:
- Clean Compressed Air: Most economical solution for general mild steel up to 25 mm. Requires multi-stage filtration to eliminate moisture and oil droplets down to 0.01 microns to prevent premature torch electrode cratering.
- Pure Oxygen (O2): Used as the plasma gas for carbon steel to induce an exothermic reaction, boosting cutting speeds by up to 25% while producing smooth, dross-free bottom edges ready for automated painting.
- Nitrogen (N2): Primary choice for stainless steel and aluminium. Nitrogen prevents oxidation, producing shiny, corrosion-resistant edges suitable for food-grade, pharmaceutical, and marine vessels.
- H35 / F5 Gas Mixtures (Argon-Hydrogen / Nitrogen-Hydrogen): Recommended for heavy stainless steel (>20 mm). The high thermal conductivity of hydrogen imparts extreme heat into thick sections, blowing out molten metal cleanly without dross attachment.