Featured High-Precision Orbital & Industrial Welders
Explore our export-grade orbital GTAW, handheld fiber laser, and automated pipe welding solutions designed for zero-defect radiographic joinery across pharmaceutical, semiconductor, and aerospace sectors.
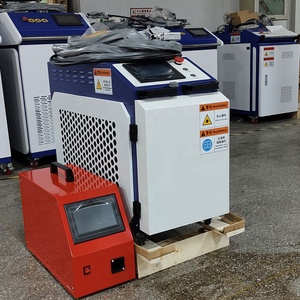
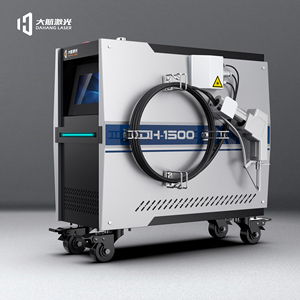
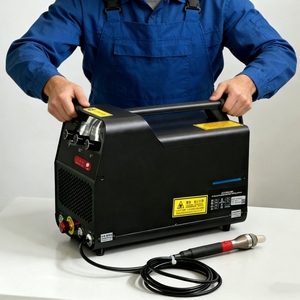
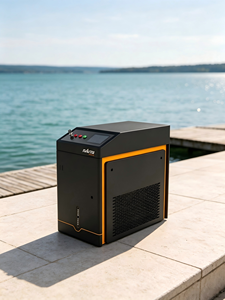
All-in-One Design Handheld Laser Welder Chiller SY-1500 System
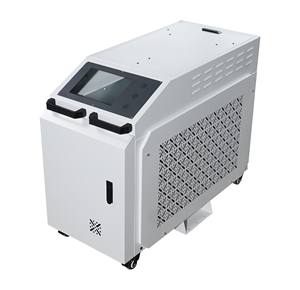
4-in-1 Air-Cooled Laser Steel & Aluminum Welding Equipment
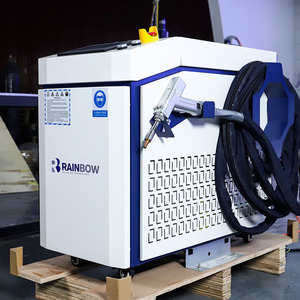
PANGOLIN High-Efficiency Fiber Laser Welding System (1000W-3000W)
Portable 600W Mini Handheld Spot & Orbital Tube Micro Welder
Industrial Production Laser & Orbital Welder (1500W-3000W)
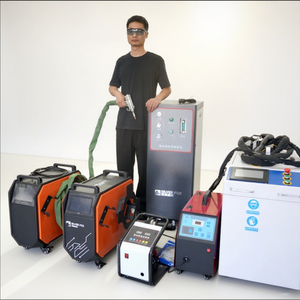
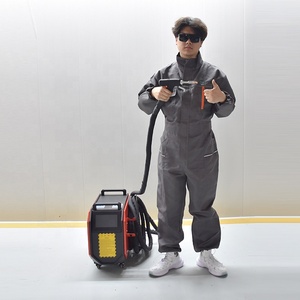
Outdoor Portable 4-in-1 Orbital & Laser Pipeline Welding Station
1500W Fiber Laser & Automated Orbital Welding System Package
The Engineering & Arc Metallurgy of Modern Orbital Welding
An in-depth analysis of Gas Tungsten Arc Welding (GTAW) mechanics, oxygen purge dynamics, and thermal energy modulation in closed-chamber orbital joins.
Precision Closed-Chamber vs. Open-Head Orbital Dynamics
Orbital welding represents the highest echelon of automated precision joinery. By rotating an arc 360 degrees around a static tube or pipe workpiece, orbital GTAW eliminates human operator variance, delivering 100% repeatable, radiographic-quality weld beads. The primary engineering distinction lies between closed-chamber weld heads and open-frame orbital heads.
Closed-chamber heads completely enclose the joint in an inert atmosphere (typically 99.999% pure Argon or Argon-Hydrogen mixtures). This total atmosphere isolation prevents atmospheric oxidation of reactive metals such as 316L Stainless Steel, Titanium, and Hastelloy during the molten liquid phase. Conversely, open-frame heads utilize targeted gas lenses for larger diameter structural piping, offering modular wire feeding mechanisms and multi-pass capability for heavy-wall schedules.
- Current Pulsing Waveforms: High-frequency synchronized pulse modulation (0.5 Hz to 200 Hz) synchronizes peak current with electrode positioning to freeze the weld pool, avoiding gravity-induced sag during overhead (12 o'clock to 6 o'clock) orbital passes.
- Purge Oxygen Thresholds: Maintaining residual oxygen levels under 5 PPM inside the tube ID prevents internal root discoloration ("sugaration") without requiring toxic chemical passivation post-weld.
- Thermal Input Equation: Precise digital control of travel speed ($v$) and arc current ($I$) guarantees exact heat input ($Q = \frac{V \times I \times 60}{v \times 1000} \times \eta$), keeping the heat-affected zone (HAZ) ultra-narrow and preventing chromium carbide precipitation.
Global Procurement Trends: Orbital Welding Systems (2025–2030)
How semiconductor cleanrooms, biopharmaceutical standards, and Industry 4.0 digitizing are reshaping global B2B procurement requirements for orbital equipment.
ASME BPE & Semiconductor UHP Compliance
Global procurement in the bioprocess and semiconductor sectors now strictly demands compliance with ASME BPE SD-3.8 guidelines. Procurement managers are prioritizing orbital suppliers offering integrated oxygen sensors, digital trace logs, and seamless purge pressure monitoring to guarantee root penetration profiles under Ra 0.25 µm smooth finish standards.
IoT Data Logging & Traceability
Modern orbital welding power supplies are transitioning from standalone units to networked IoT nodes. Export-ready systems must automatically export real-time voltage, current, motor torque, and purge gas flow rate records for every single joint directly to cloud MES (Manufacturing Execution Systems) via OPC-UA protocols for 100% auditability.
Fiber Laser & Orbital Hybrid Systems
The convergence of fiber laser light sources and automated orbital rotation represents the next technological boundary. Laser orbital heads achieve penetration speeds up to 10 times faster than traditional GTAW on thick-walled aerospace tubing while drastically lowering total heat input and minimizing structural distortion.
Technical Benchmarking: Orbital GTAW vs. Handheld Laser vs. Manual TIG
A comparative engineering matrix aiding technical buyers in evaluating cycle efficiency, thermal impact, radiographical compliance, and operational capital expenditure.
| Performance Metrics | Closed-Chamber Orbital GTAW | Handheld / Orbital Laser | Manual TIG Welding | ARC (SMAW) Heavy Duty |
|---|---|---|---|---|
| Radiographic Pass Rate | > 99.8% (Class 1 Quality) | > 98.5% (High Precision) | 85% – 92% (Operator Dependent) | 80% – 88% (Requires Slag Grinding) |
| Travel Speed / Deposition | 100 – 250 mm/min | 500 – 1500 mm/min | 30 – 80 mm/min | Moderate (High Deposition Rate) |
| Heat-Affected Zone (HAZ) | Very Narrow & Controlled | Ultra-Narrow (< 0.5 mm) | Wide (Risk of Thermal Distortion) | Extremely Wide |
| Purge Gas Dependency | Mandatory (< 5 PPM O2 Target) | Recommended for Stainless | Mandatory for Stainless Tube | Not Required |
| Skill Requirement | Programmer / Technician | Minimal (Semi-Automated) | High Skilled Welder Needed | Standard Craftsman |
| Target Applications | Pharma, High-Purity Gas, Aerospace | Sheet Metal, Enclosures, Auto Lines | Custom Shop Repair, Jobbing | Structural Steel, Shipyards, Heavy Engineering |
Enterprise Advantage & Manufacturing Excellence
Built upon six decades of precision electrical engineering, rigorous load testing, and uncompromised quality assurance for global export markets.
Why Global Engineering Procurement Teams Trust Our Supply Chain
Our manufacturing philosophy centers on industrial robustness and severe-duty performance. Unlike light-duty commercial welders, every industrial power source, orbital motor drive, and fiber laser unit is built for continuous 100% duty cycle operational stress.
- Class F/H Copper Insulation: In-house winding of transformers and chokes utilizing high-grade Class H copper insulation rated for temperatures up to 180°C, delivering immune performance against mains power fluctuations.
- 100% Full-Load Pre-Dispatch Testing: Every machine undergoes a 4-hour burn-in and full-load thermal endurance test prior to export packaging. Serial-matched test certificates are archived for full warranty traceability.
- Direct OEM Customization: We offer custom torch lead lengths, water-cooled orbital head packages, custom trolley mounts, dual voltage setups (220V/380V/440V 50-60Hz), and dedicated CNC cutting table sizing.
- Global Logistics Ready: Heavy-duty sea-worthy crating with vacuum desiccant wrap guarantees zero moisture corrosion during multi-week oceanic freight shipments.
Serving Critical High-Purity & Heavy Engineering Industries
From ultra-clean bioprocess piping to heavy structural steel, our welding technology drives critical global infrastructure.
Pharmaceutical & Biotechnology
Ultra-clean sanitary tubing (316L EP), WFI (Water For Injection) distribution loops, and fermenter vessel connections with internal mirror-smooth bead profiles.
Semiconductor Cleanrooms
Ultra-high purity (UHP) gas delivery lines utilizing 1/4" to 4" thin-wall stainless steel tubing under strict zero-particulate closed-chamber conditions.
Aerospace & Energy Heat Exchangers
Tube-to-tubesheet joint automation in high-pressure titanium condensers, boiler headers, and aerospace hydraulic distribution lines.
Procurement & Engineering FAQ
Expert technical answers to common B2B purchasing inquiries regarding orbital power sources, import standards, and parameter setup.
Which orbital and industrial welding machines does your factory export?
Our complete manufacturing range encompasses closed-chamber orbital GTAW tube welders, open-head pipe welders, 4-in-1 multi-process handheld fiber laser systems (1000W to 3000W), heavy-duty ARC (SMAW) rectifiers up to 1250A, AC/DC TIG welders, MIG/MAG synergic inverters, capacitor-discharge stud welders, and automated CNC cutting tables.
Why is closed-chamber orbital welding preferred for stainless steel tubing?
Closed-chamber orbital heads flood the complete joint exterior with inert Argon shielding gas while holding the tube perfectly aligned. This eliminates discoloration and oxidation (heavy tinting), guaranteeing zero internal sugaration and meeting strict ASME BPE standards for bioprocess lines without manual post-weld chemical cleaning.
Are your export welders compatible with international 3-phase voltages?
Yes. All export units are custom-engineered to support international industrial mains standards, including 220V single-phase, 380V, 415V, and 440V 3-phase supplies at 50 Hz or 60 Hz. Systems feature CE-compliant internal wiring, international industrial plug configurations, and thermostatic overload cutouts.
How do you guarantee 100% duty cycle under heavy industrial operation?
Heavy-duty power sources utilize heavy-gauge Class H insulated copper transformer windings, high-capacity aluminum heat sinks, and high-CFM forced-air or dual-loop water cooling channels. This allows continuous multi-shift fabrication at maximum rated current without thermal shutdown.
What technical and after-sales support is provided for overseas buyers?
Every machine export consignment includes complete electrical wiring schematics, recommended 2-year maintenance spare-parts kits, and comprehensive user operation manuals. Furthermore, our application engineers provide remote video commissioning support, PLC parameter troubleshooting, and operational training for your technical crew.
Can system parameters be customized for proprietary alloy tube jointing?
Absolutely. Our R&D team regularly programs custom pulse frequency curves, rotational speed profiles, and wire feed parameters tailored to specialized alloys such as Inconel, Monel, Hastelloy C-276, Duplex 2205, and thin-wall Titanium tubing.
Ready to Optimize Your Tube & Pipe Fabrication Quality?
Consult with our senior welding engineers today for technical machine selection, joint feasibility testing, or factory-direct export quotations tailored to your project requirements.
Contact Us