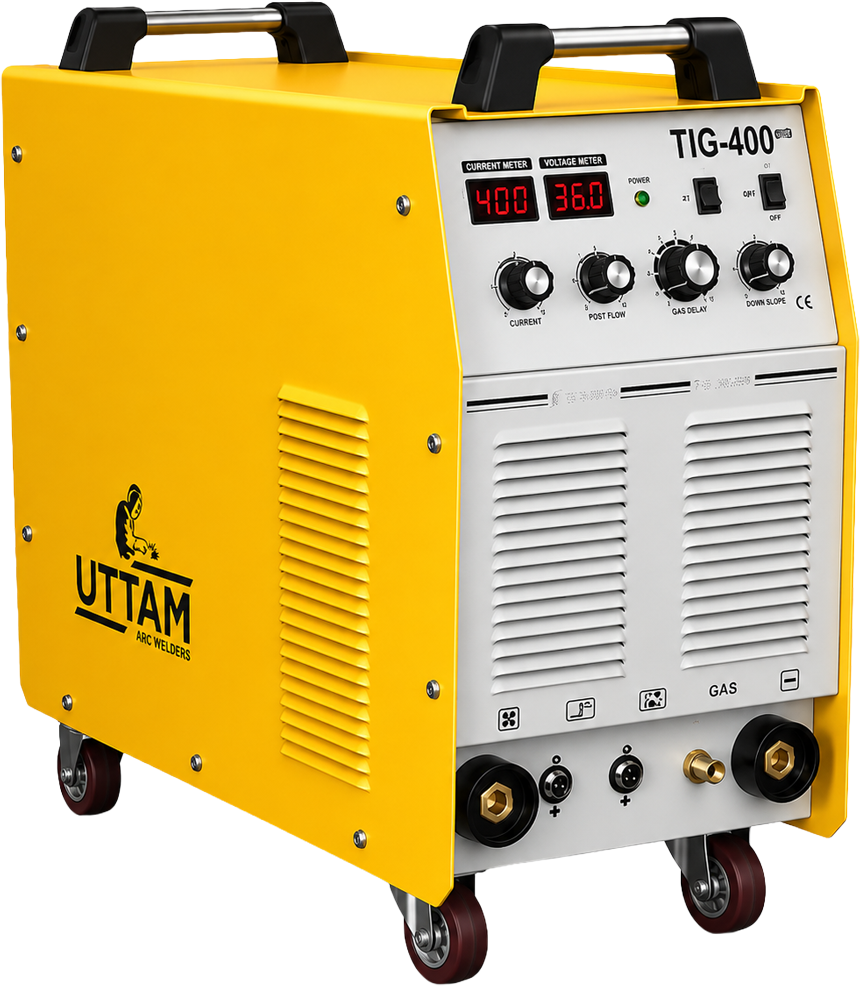
Single Holder ARC Welding Machine
A heavy-duty manual stick welding power source engineered for multi-shift industrial fabrication. Provides stepless current regulation and high arc stability across all electrode types from 2.5 mm to 6.0 mm.
Selecting an ARC welding machine (Shielded Metal Arc Welding / SMAW power source) for heavy industrial applications demands a rigorous analysis of volt-ampere dynamic characteristics, thermal overload limits, and power factor efficiencies. In heavy structural fabrication, pipeline construction, and marine engineering, SMAW remains the most versatile, weather-tolerant jointing process. However, the performance gap between consumer-grade welders and true industrial-duty power sources dictates whether a plant achieves seamless multi-shift productivity or suffers costly thermal shutdown delays.
Industrial SMAW processes rely on a Constant Current (CC) volt-ampere output curve. As the welder alters arc length during manual operation, the power source must automatically adjust voltage while keeping output amperage virtually constant. This dynamic response prevents electrode freezing (stubbing) during short-arc root passes and eliminates destructive weld pool blowout when working with aggressive flux coatings like high-cellulose (E6010, E6011) or low-hydrogen basic electrodes (E7018, E7018-1).
Understanding power conversion topologies allows procurement teams to match machinery lifespan, energy tariffs, and site mobility requirements to the correct equipment classification.
Utilizing high-frequency pulse-width modulation (PWM) through Insulated Gate Bipolar Transistors operating between 20kHz and 50kHz, IGBT inverter arc welders step down voltage with a fraction of the core size required by conventional 50Hz transformers.
Primary Strategic Advantages:
Combining heavy-gauge electrolytic copper magnetic coils, grain-oriented silicon steel cores, and heavy silicon rectifier diodes (SCR), traditional ARC welding rectifiers remain unmatched in absolute mechanical ruggedness.
Primary Strategic Advantages:
Engineered in India and exported worldwide. Every machine specification below reflects industrial heavy-duty rating standards with fully customizable input voltage, duty cycle, and torch packages.
A heavy-duty manual stick welding power source engineered for multi-shift industrial fabrication. Provides stepless current regulation and high arc stability across all electrode types from 2.5 mm to 6.0 mm.
Houses two completely isolated, independently regulated welding circuits within a single compact chassis. Allows two operators to weld simultaneously off one power point without mutual arc interference.
Built for extreme duty cycles in heavy engineering bays. Delivers smooth DC current output up to 1250 A, ideal for heavy-plate jointing, carbon arc gouging, and hardfacing applications.
High-efficiency synergic power source capable of switching seamlessly between MIG wire feeding, flux-cored welding, and heavy manual ARC (SMAW) modes with a single button press.
Delivers clean, high-speed severance of conductive alloys, structural carbon steel, stainless steel, and aluminum plate with a narrow heat-affected zone and minimal dross formation.
State-of-the-art fiber laser welding sources and automated CNC plate cutting tables designed for high-speed, distortion-free manufacturing of sheet metal assemblies and precision components.
Use this engineering matrix to evaluate primary power input, duty cycle ratings, open-circuit voltage (OCV), and electrode compatibility for your specific production environment.
| Model Series | Max Output | Duty Cycle @ 40°C | OCV (Volts) | Electrode Dia. Range | Primary Voltage Input | Core Heavy Application |
|---|---|---|---|---|---|---|
| ARC-200 HD | 200 Amps DC | 60% @ 200A / 100% @ 155A | 78V | 2.0 mm – 3.25 mm | 220V 1-Phase / 380V 3-Phase | Light structural, site maintenance, repair workshops |
| ARC-310 HD | 300 Amps DC | 60% @ 300A / 100% @ 230A | 82V | 2.5 mm – 4.0 mm | 380V / 415V / 440V 3-Phase | Medium fabrication, architectural steelwork, piping |
| ARC-400 HD | 400 Amps DC | 60% @ 400A / 100% @ 310A | 85V | 2.5 mm – 5.0 mm | 380V / 415V / 440V 3-Phase | Heavy structural steel, pressure vessels, erection site |
| DH-400 x 2 (Twin) | 400A x 2 Dual | 60% per holder simultaneous | 80V per holder | 2.5 mm – 5.0 mm | 380V / 415V / 440V 3-Phase | Shipyard staging, structural steel construction bays |
| RECT-600 HD | 600 Amps DC | 100% Continuous @ 600A | 88V | 3.15 mm – 6.3 mm | 380V / 415V / 440V 3-Phase | Mining repair, carbon arc gouging, hardfacing |
| RECT-1250 SAW | 1250 Amps DC | 100% Continuous @ 1250A | 92V | 4.0 mm – 10.0 mm / SAW Wire | 380V / 415V / 440V 3-Phase | Heavy foundry engineering, submerged arc welding |
Operational feedback from heavy engineering fabricators, pipeline contractors, and automated production shops globally.
Engineered to deliver unbroken arc characteristics across extended welding cable runs up to 100 meters. Built with dynamic arc force controls that compensate for voltage drop, allowing welders to maintain high-integrity root beads in restricted access joints.
Delivers clean, low-dross thermal cutting on carbon steel, stainless steel, and aluminum plates up to 40 mm thick. Reduces downstream edge grinding costs by up to 65% compared to oxy-fuel flame cutting methods.
Provides ultra-fast travel speeds—up to 4x to 10x faster than TIG—with negligible thermal distortion. Enables ultra-thin sheet metal jointing with pristine cosmetic finishes that require no post-weld polishing.
Industrial plate cutting automation designed for high-yield nested profiling. Heavy-duty double-side gantry drives preserve repeat positioning tolerances under continuous multi-shift production schedules.
How digital power conversion, green energy compliance, and remote site requirements are reshaping B2B welding equipment purchasing strategies worldwide.
Industrial electricity tariffs and carbon intensity regulations are driving global fabrication yards away from traditional transformer welders toward Active Power Factor Correction (PFC) Inverter ARC welding machines. Operating at power factors above 0.95, PFC-equipped inverters draw up to 35% less kVA current from local utility mains, enabling plants to operate more machines on existing transformer sub-stations while eliminating low-power-factor penalty surcharges.
Cross-country pipeline installation, offshore wind turbine erection, and remote mining sites rely exclusively on diesel generator power. Future-ready ARC welders incorporate wide input voltage tolerance bands (spanning 300V to 480V 3-phase). Advanced primary sensing automatically compensates for generator frequency hunting and momentary voltage sags, eliminating arc instability and thermal inverter shutdown.
As the shortage of certified manual welders persists globally, purchasing managers are specifying ARC welding machines equipped with intelligent wave-process algorithms. Modern digital arc force control automatically detects short-circuit micro-droplets and injects precise current surges within microseconds. This prevents stick electrode freezing, reduces spatter by over 40%, and enables less-experienced operators to pass radiographic X-ray weld inspections.
Enterprise procurement teams are increasingly calculating Total Cost of Ownership (TCO) over a 10-year horizon rather than focusing solely on initial acquisition cost. Key procurement trends emphasize modular inverter board layouts, standardized replacement components, potted electronics for IP23 moisture and dust protection, and guaranteed long-term spare parts availability from original equipment manufacturers (OEMs).
When procuring ARC welding machines for international export projects, confirm that the manufacturer provides factory-tested voltage configuration options (such as 380V 50Hz for Europe/Asia, 415V for Commonwealth regions, or 440V/480V 60Hz for Americas/Middle East). Ensuring native transformer taps or wide-band inverter tolerance prevents costly field transformer retrofits.
For six decades, Uttam Industries has served as a cornerstone manufacturer and exporter of heavy industrial welding equipment. Operating out of manufacturing complexes in Mandi Dabwali (Haryana) and Delhi, India, our engineering philosophy prioritizes heavy thermal design margins, mechanical longevity, and transparent technical specifications over cheap component compromises.
Our practical shop-floor heritage working alongside structural steel fabricators, railway workshops, foundries, and shipyards ensures every machine design addresses real-world welding challenges:
Different industrial sectors require distinct duty cycles, arc force dynamics, and mechanical mobility options. We configure machines tailored to sector-specific standard compliance.


Technical, commercial, and operational insights answered by Uttam Industries' chief welding engineers.
Industrial-grade ARC welding machines (SMAW) are categorized by their ability to operate under continuous duty cycles (60% to 100% at maximum rated current) under ambient temperatures of 40°C. Key engineering hallmarks include Class H copper-wound transformer insulation, an elevated Open-Circuit Voltage (OCV between 75V and 90V DC) for reliable arc initiation with basic and cellulosic electrodes (E6010, E7018), thermostatic overload safety cut-outs, forced-air cooling ducts, and an IP23 enclosure rating for outdoor site protection.
Unlike light commercial units that suffer duty cycle drop-offs under ambient heat, industrial power sources from Uttam Industries utilize thick-section copper magnet wire and high-thermal-capacity iron cores, ensuring consistent current delivery during multi-shift continuous welding operations.
Duty cycle is defined by international standard IEC 60974-1 as the percentage of a 10-minute operational block during which an ARC welding machine can deliver its rated current without exceeding internal thermal limits at 40°C ambient temperature. For example, a 60% duty cycle rating at 400A means the machine can weld continuously for 6 minutes at 400A, followed by 4 minutes of cooling fan operation.
To calculate duty cycle at lower operating currents, use the mathematical formula: Duty Cycle % (at I₂) = Rating Duty Cycle % × (I₁ / I₂)². For instance, an ARC welder rated 60% at 400A will achieve near 100% continuous duty cycle when operated at 310A output, making it ideal for continuous structural welding using 4.0 mm electrodes.
A Double Holder ARC welding machine integrates two completely isolated, independently regulated DC output circuits within a single heavy-duty chassis powered by a shared high-efficiency magnetic transformer core. This architecture offers major operational advantages for shipyards, bridge assembly yards, and structural steel shops:
Open-Circuit Voltage (OCV) is the voltage measured across the electrode holder and work clamp when the welder is energized but no arc is present. High OCV (75V–90V) is essential when running specialized flux-coated electrodes such as cellulosic E6010 or E6011 (commonly used for root pass pipeline welding) and low-hydrogen basic rods like E7018-1.
Cellulosic coatings require high electrical pressure to ionize the arc gap quickly upon contact. If an ARC welder's OCV is too low (below 60V), operators experience erratic arc strikes, excessive arc stubbing, porous weld starts, and potential X-ray fault inclusions in structural butt welds.
Yes. All Uttam industrial ARC welding machines are engineered specifically for demanding site conditions where primary mains voltage fluctuates or power is supplied by engine-driven diesel generators. Our transformer rectifiers feature wide primary voltage taps (±15% to ±20% tolerance), while our IGBT inverter power sources incorporate active input filter capacitors and transient voltage suppressors (TVS).
This protection buffers sensitive internal diodes and IGBT gates against line voltage spikes, neutral floats, and frequency variations typical of remote construction sites, ensuring reliable arc maintenance without component failure.
As a direct manufacturer and exporter, Uttam Industries customizes primary transformer windings and power electronics for global electrical standards. Supported configurations include:
Machines are supplied with clearly labelled terminal blocks, CE-compliant wiring color codes, and multilingual operating manuals.
Transformer insulation class dictates the maximum allowable operating temperature of the magnetic wire coils. Class H insulation is rated for operating temperatures up to 180°C (compared to standard Class F rated at 155°C or Class B at 130°C). By utilizing 99.9% pure electrolytic copper wire wound with double-polyester glass yarn and vacuum pressure impregnated with high-grade varnish, Uttam ARC welders withstand intense thermal cycling without insulation carbonization.
This prevents internal inter-turn short circuits, maintains electrical efficiency over decades of hard use, and lowers Total Cost of Ownership (TCO) by eliminating costly transformer rewinding expenditures.
Every export shipment from Uttam Industries undergoes a multi-stage Quality Inspection Protocol. Customers receive a factory test report detailing open-circuit voltage checks, full-load current calibration, insulation resistance testing (at 2.5kV AC for 1 minute), and temperature rise verification linked to the machine's serial number.
For international transit, machines are enclosed in heavy-duty sea-worthy wooden crates with internal polyethylene vapor barriers and moisture-absorbing desiccant pouches. Complete wiring diagrams, spare parts catalogs, and operator safety manuals are enclosed in every shipping crate.
Share your required base material grades, joint thicknesses, electrode diameters, and site power supply—our engineering team will recommend the exact ARC welding machine topology, output rating, and duty cycle class for your project.